Plastic bag making machine troubleshooting

The most common problems with plastic bag machine

Plastic Bag Machine is the final step in the manufacturing and processing of plastic bag. If the performance of bag making process isn’t high enough or the quantity of waste is excessive, the previous processes , such as blowing film machine or composite printing machine could end up being used up and downstream customers are likely to have an enormous effects on the manufacturing and operations.

1. What can I do if my bag’s contents leak or become damaged because of the insufficient sealant of the plastic bag machine?
Cause: Low anti-pollution heat-sealability for the film, mostly due to the resin that is used in the sealing layer isn’t suitable for.
Countermeasures: Select a film that has excellent anti-pollution heat-sealability. The general rule is that ldpe has moderate anti-pollution heating capacity. EVA is a good anti-pollution heat sealability in the event that the VA contents are large. Ionic resin and metallocene-based polymer It is extremely effective in preventing pollution heat-sealability.

2.What can I do when the seal of the plastic bag machine isn’t as strong?

 Reasons:
1. The temperature of heat sealing is too high.
2. Pressure is too high.
3. The time to seal heat is too long.
4. Edge of upper portion of the sealer sharp or coating is damaged.
5. The seal at the bottom is Silicone rubber that is too for the job;
6. During the process of compounding and curing during the curing and compounding process, a portion of the adhesive gets absorbed into the film. When the substrate is impacted by the adhesive. The hardness (that is, resistance to impact) is reduced and the brittleness grown;
7 polymer composite bags for packaging Following cooling and putting in place the bags in the heat seal is increased as well as it tends to soften.

Countermeasures:

1. Based on the characteristics of heat sealing of the inner sealing material, select the proper temperatures, pressure, and time for heat sealing;

2. Improve the condition of the surface of the top heat sealing knife, making the sealer’s surface smooth;

3. Cover with polyethylene cloth cover is intact.

4. Select a rubber pad made of silicone that is of the right degree of hardness.

What can I do if my bag starts to shrink after being sealant by the bag-making machine?
The reason:
1. Its thickness in the composite film appears not uniform;
2. The temperature of heat sealing is too high, or the time for heat sealing will be long.
3. In the heat sealing knife’s longitudinal section The running path of composite films isn’t straight.
4. Insufficient cooling.
5. The time for curing isn’t enough.
6. The film that covers the surface of the substrate is not very resistant to heat.
7. Inadequate control of the tension match on the surface of the composite film during the process of compounding can result in residual stress after curing and setting. This is especially true because the film is less and such failures are more likely to occur.
Countermeasure
1. The tension can be adjusted on the roller floating.
2. Utilize an inner sealing base material that has low temperature heat sealability.
3. Adjust the temperature of the heat seal to the appropriate temperature.
4. It is important to cool down.
5. Create a film that is mature.
6. Re-select the film on the surface.
7. Adjust the tension on each component of the composite processing equipment, and then try to ensure that both substrates shrink the same.

What can I do if I notice that the outer shape of the heat-sealed exterior of the plastic bag making machine isn’t clear after sealing? (The knife’s pattern isn’t transparent)
The reason is:
1. The cooling process is short.
2. The cooling plate is not in good contact with the plate
3. When the pad of silicone is heated, the edges melt.
4. Forces of heat sealing in the longitudinal direction that are not balanced
5. Edge of heat sealing knife is uneven and sharp.
Countermeasure
1. Change the cooling duration.
2. Adjust the cooling plate to your liking.
3. Adjust or replace the knife that seals heat
4. Stop the melting of the edges caused by the overheating of silicon pad.

What can I do if the sealing power of the bag making machine is weak after sealing?
the reasonfor this:
1. The adhesive contained in the composite film hasn’t been sufficiently cured.
2. The conditions for heat sealing are not appropriate.
3. Between the knife that seals the temperature and the cooling knife is too long.
4. There is an issue with the outer layer of sealing.
5. The ability to seal heat in the ink is not as strong, which results in a reduction in the strength of the composite of the film on the part that is sealed with heat.
6. Dust and spray powders as well as other substances stick with the heat of the covers.
7. The strength of the composite is not high or the strength of the heat sealed place is reduced too much.

Countermeasures:
1. Help to promote the hardening process of adhesive (curing or curing) by conserving heat and aging. This will improve the strength and resistance to heat of the film.
2. Find the ideal conditions for heat-sealing (temperature time, pressure and temperature) in accordance with the structure that the film has, the its heat-sealing state and so on. You can also enhance the method of heat-sealing, and then cool down right away after the heat-sealing process.
3. Examine the shelf condition and shelf life of the film that is heat-sealable. If the film that is heat-sealable uses the older batch of film and is the same film has been sealed needs special attention.
4. The thickness of the film that can be heat-sealable.
5. Modify the type and the grade of the film that can be heat-sealable and choose a film that has anti-pollution heat-sealability.
6. Make sure the quality of the adhesive meets standards (the release of low-molecular substances within the resin could influence its composition)
7. Improve the heat sealing efficiency for the layer of heat. regulate the contents of the slip agents and make use of the mlldpe film.
8. Monitor the monomer concentration that is present in MDI inside the adhesive.

What can I do if there are air bubbles and uneven surfaces appear in the heat-sealed area of the bag maker machine?
The reason is:
1. If heat-sealing takes place on an object made up of hygroscopic material like nylon film, the hygroscopic film can create air bubbles after the film absorbs water.
2. The heat-sealing knife , or the heat-sealing pad of silicone is not even.
3. Insufficient pressure for heat sealing.
4. Utilizing one-component adhesives like neoprene, when sealing bags with heat are used, the heat cover can be prone to pits.
Countermeasures:
1. Make sure to store the raw materials and semi-finished goods in a proper manner to prevent water absorption.
2. Adjust or check your heat sealing blade or the heat sealing pad.
3. Removing the glue tape.

If you need any information of blown fim extrusion,plastic bag machine,printing machine,please feel free to contact us. Kingdom Machine Factory  Mobile:0086-13088651008;0086-13958812663;
Whatsapp/Viber/Tango:0086-13088651008;0086-13958812663;
sale@kingdommachine.com;kingdombillwang@hotmail.com; www.blownfilmextrusion.com; www.kingdommachine.com;
Ruian Economic Zone,Wenzhou,China
Plastic bag making machine troubleshooting

Plastic bag making machine problem solution in Dubai,Ajman,Umm al-Quwain,Abu Dhabi,Sharjah,Fujairah,United Arab Emirates 

Plastic Bag Machine is the final step in the manufacturing and processing of plastic bag. If the performance of bag making process isn’t high enough or the quantity of waste is excessive, the previous processes , such as blowing film machine or composite printing machine could end up being used up and downstream customers are likely to have an enormous effects on the manufacturing and operations.

1. What can I do if my bag’s contents leak or become damaged because of the insufficient sealant of the plastic bag machine?
Cause: Low anti-pollution heat-sealability for the film, mostly due to the resin that is used in the sealing layer isn’t suitable for.
Countermeasures: Select a film that has excellent anti-pollution heat-sealability. The general rule is that ldpe has moderate anti-pollution heating capacity. EVA is a good anti-pollution heat sealability in the event that the VA contents are large. Ionic resin and metallocene-based polymer It is extremely effective in preventing pollution heat-sealability.

2.What can I do when the seal of the plastic bag machine isn’t as strong?

Video of plastic bag machine

Reasons:

1. The temperature of heat sealing is excessively high.
2. The pressure is too high.
3. The time to seal heat is too long.
4. Edge of upper section of the sealer sharp or the PTFE coating is damaged.
5. The seal on the bottom is Silicone rubber that is too for the job;
6, in the process of compounding and curing during the curing and compounding process, a portion of the adhesive gets absorbed into the film. When the substrate is impacted by the adhesive. As a result, the hardness (that is, resistance to impact) has diminished and the brittleness grown;
7 Plastic composite baggies for packing Following cooling and putting in place the bags, the durability of the heat seal improves and the bag also begins to harden.

Countermeasures:

1. Based on the heat sealing properties of the outer sealing layer material, choose the right temperatures, pressure, and time to seal the heat;

2. Improve the surface quality of the top heat sealing knife so that it makes the sealer’s surface smooth;

3. Wrap the cloth with polyethylene. The wrapping is still intact.

4. Select a pad made of silicone that is of the right degree of hardness.

What can I do if my bag starts to shrink after being sealant by the bag maker?
The reason:
1. The film’s thickness is variable;
2. The temperature for heat sealing is too high, or the time to seal can be too lengthy.
3. In the heat sealing knife’s longitudinal section The running path of composite films isn’t straight.
4. Insufficient cooling.
5. The time for curing isn’t enough.
6. The film on the surface is not very resistant to heat.
7. Inadequate control of the tension-matching to the substrate of the composite during the process of compounding causes residual stress following curing and setting, particularly in cases where the composite film is smaller this type of failure is more likely to occur.
Countermeasure
1. The tension can be adjusted on the roller floating.
2. Utilize an inner sealing base material that has low temperature heat sealability.
3. Adjust the temperature of the heat seal to the appropriate temperature.
4. It is important to cool down.
5. Create a film that is mature.
6. Re-select the film on the surface.
7. Adjust the tension on each component of the composite processing equipment, and then try to ensure that both substrates shrink the same.

What can I do if I notice that the outer shape of the heat-sealed exterior of the bag-making machine isn’t clear after sealing? (The knife’s pattern isn’t evident)
The reason is:
1. The cooling process is short.
2. The cooling plate is not in good contact with the plate
3. When the pad of silicone is heated, the edges melt.
4. Forces of heat sealing in the longitudinal direction that are not balanced
5. Its edge on the heat sealing knife is sloping and blunt.
Countermeasure
1. Set the cooling time.
2. Adjust the cooling plate to your liking.
3. Adjust or replace the knife that seals heat
4. Avoid melting at the edge due to overheating of the silicon pad.

What can I do if the sealing capacity of the bag maker is weak after sealing?
the reasonfor this:
1. The adhesive contained in the composite film hasn’t been properly cured.
2. The conditions for heat sealing are not appropriate.
3. Between the knife that seals the temperature and the cooling knife is too long.
4. There is an issue with the inner layer of sealing.
5. The ink’s heat-sealability is weak, resulting in a reduction in the strength of composites of the film in the sealed part.
6. Dust and spray powders as well as other substances stick on the cover.
7. The strength of the composite is not high or the strength of the heat sealed place decreases too much.

Countermeasures:
1. Help to promote the hardening process of adhesive (curing or curing) by preserving heat and aging. This will improve the strength and resistance to heat of the film.
2. Find the ideal conditions for heat-sealing (temperature as well as time and pressure) in accordance with the structure of the material, its heat-sealing state and so on. Or, you can enhance the method of heat-sealing, and then cool down right away after the heat-sealing process.
3. Examine the shelf time and storage conditions of the film that is heat-sealable. If the film is made of the film from the previous batch and also the film has been sealed with heat requires special attention, it is recommended to do so.
4. The thickness of the film that can be heat-sealable.
5. Modify the type and the grade of the film that can be heat-sealable and choose a film that has anti-pollution heat-sealability.
6. Verify that the quality of the adhesive meets standards (the release of low-molecular substances in the resin can alter how the glue is made)
7. Improve the heat sealing efficiency in the layers of heat. regulate the contents of the slip agents and utilize the mlldpe film.
8. Monitor the monomer concentration in MDI within the composite adhesive.

What can I do if the formation of air bubbles, or uneven surface are found in the heat-sealed area of the bag-making machine?
The reason:
1. When heat-sealing is applied to an object made up of hygroscopic material like nylon film the hygroscopic film can create air bubbles after it is absorbed by moisture.
2. The heat-sealing blade or pad of silicone is not even.
3. Insufficient pressure for heat sealing.
4. One-component adhesives, like neoprene adhesives when sealing bags with heat are used, the heat cover can be prone to pits.
Countermeasures:
1. Make sure to store the semi-finished and raw materials in a proper manner to prevent the absorption of moisture.
2. Make sure to adjust or test or adjust the knife for heat sealing as needed and the heat sealing pad.
3. Remove the tape.

If you need any information of blown fim extrusion,plastic bag machine,printing machine,please feel free to contact us. Kingdom Machine Factory  Mobile:0086-13088651008;0086-13958812663;
Whatsapp/Viber/Tango:0086-13088651008;0086-13958812663;
sale@kingdommachine.com;kingdombillwang@hotmail.com; www.blownfilmextrusion.com; www.kingdommachine.com;
Ruian Economic Zone,Wenzhou,China

Plastic bag machine

Automatic Plastic Shopping Bag Machine

Automatic Plastic Shopping Bag Machine

http://www.youtube.com/watch?v=gfycwA9kOck&feature=youtu.be

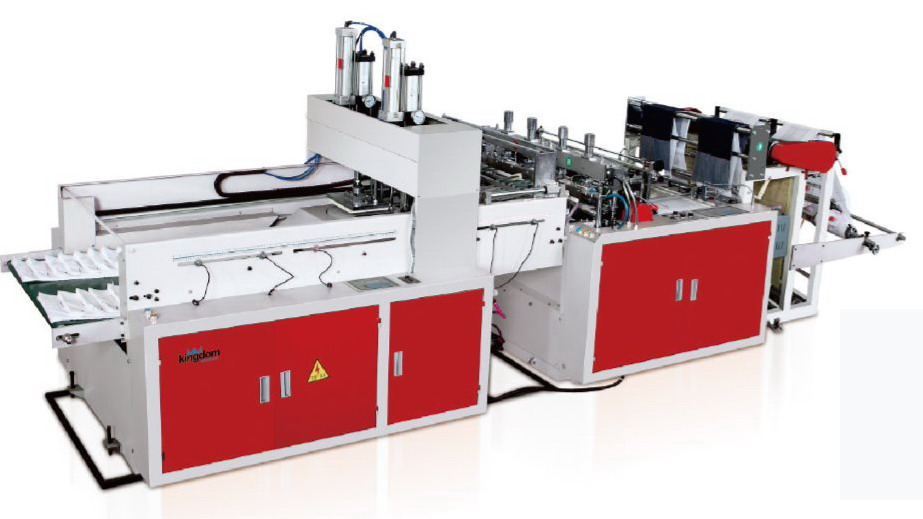
Plastic Bag Machine is applied to manufacturing and printing the uncolored vest bags(shopping bag) made of HDPE, LDPE roll plastic film. It adopts PLC control, double step motor fixed length and the liquid crystal touch screen actual display to finish the feeding, sealing, cutting, punching holes and transporting only in one process. It is of high degree of automation and good economic result.

This machine with two photocell,two driver,two knife,can make two different bag at same time.

Plastic shopping bag  
Main Technical Variables:    Model DFHQ-350*2 DFHQ-450*2 Max. Bag-making width 300mm*2 400mm*2Max.Bag-making length 600mm 600mm Bag-making thickness 0.015-0.035mm 0.015-0.035mm Bag-making speed 140-200pcs/min*2 140-200pcs/min*2 Air pressure 5kg/cm2 5kg/cm2 Total Power 7kw 9kw Weight of machine 1400kg 1600kg Overall dimensions 6000*1400*1600mm 6000*1600*1600mm

Kingdom Machine co,ltd Mobile::0086-13088651008 
Mobile: 0086-13566179950 Tel.:0086-577-65127709 
Fax:0086-577-56848008 kingdombillwang@yahoo.com
sale@kingdommachine.com  
Skype:kingdombillwang 
http://www.blown-film-extruder.com
Ruian Economic Zone,Wenzhou,China 325200